
Cast Iron & Sand Casting Cleaning
Electrolytic Removal of Sand, Scale & Graphite
Kolene® Kastech® Electrolytic is a fast, efficient, and cost-effective process for cleaning iron sand castings.
Kastech Electrolytic is chemically neutral without applied direct current. When current is applied, the workpiece is oxidized during anodic cycles and reduced during cathodic cycles. Appropriate polarity and processing time remove graphite, scale, and burned-in sand from external surfaces and internal passages.
The process is also effective in preparing iron surfaces for brazing or babbitting.
Castings are racked or fixtured so the salt reaches every internal passage (no air pockets) for complete cleaning, and so all molten salt drains freely out of the castings after processing.
Sand removal
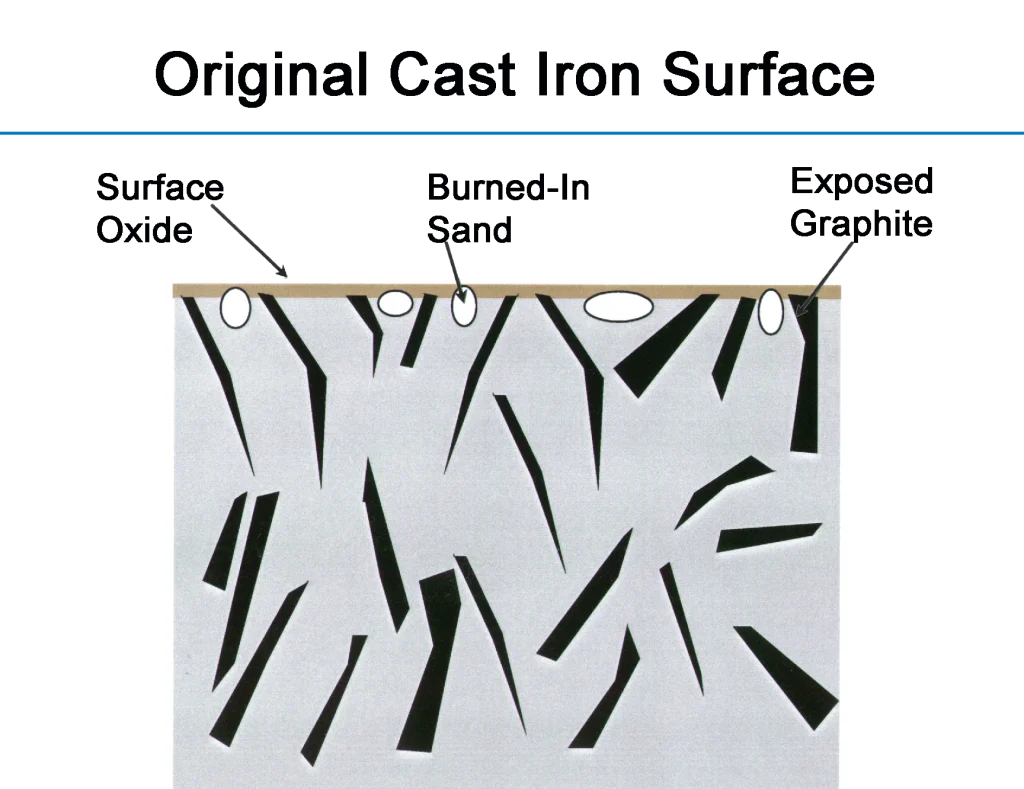
After mechanical shake-out, residual sand may remain in internal passages. Critical components such as hydraulic or pneumatic valves and cylinders can fail when remaining sand breaks free. Scoring of seals and spindles can quickly destroy the components. As-cast scale and oxide can impede good thermal transfer, especially important in engine heads and blocks.
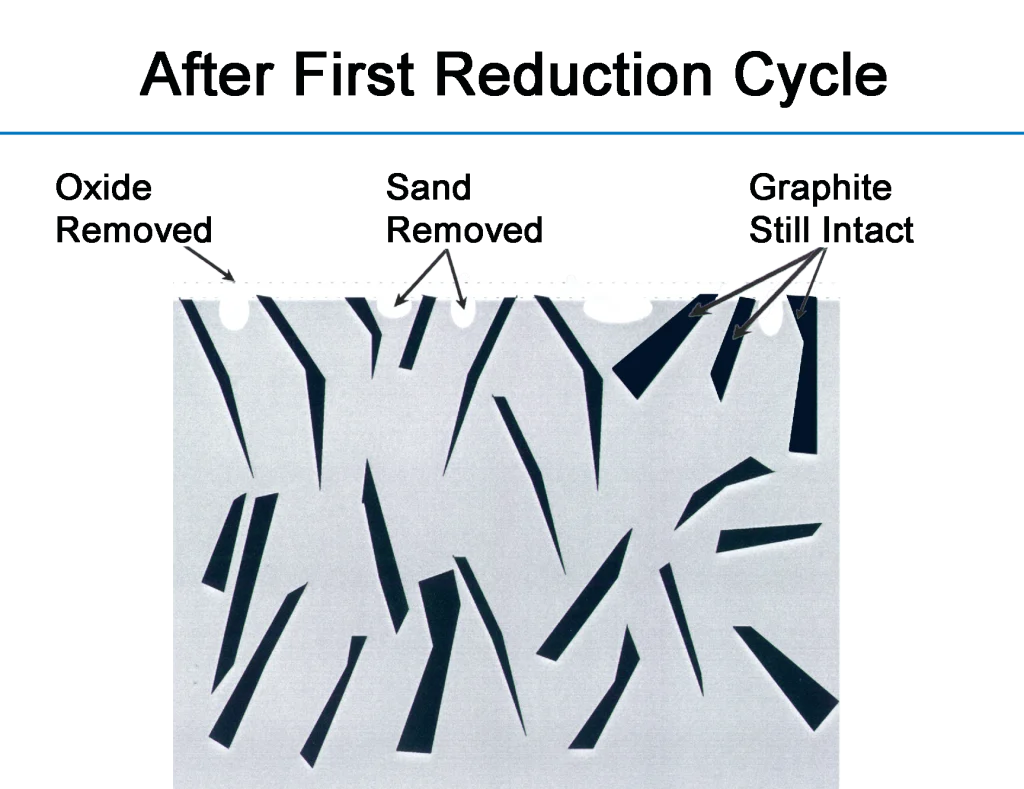
Both sand and scale can be removed with a simple reducing cycle in the Kastech Electrolytic process. Surface scale is chemically reduced, helping to expose burned-in sand. The electrolysis helps to quickly dissolve any exposed sand. Treatment time depends on the amount of scale, sand, and graphite to be removed. Scale removal also helps to improve machine tool life during subsequent machining.
Brazing or babbitting
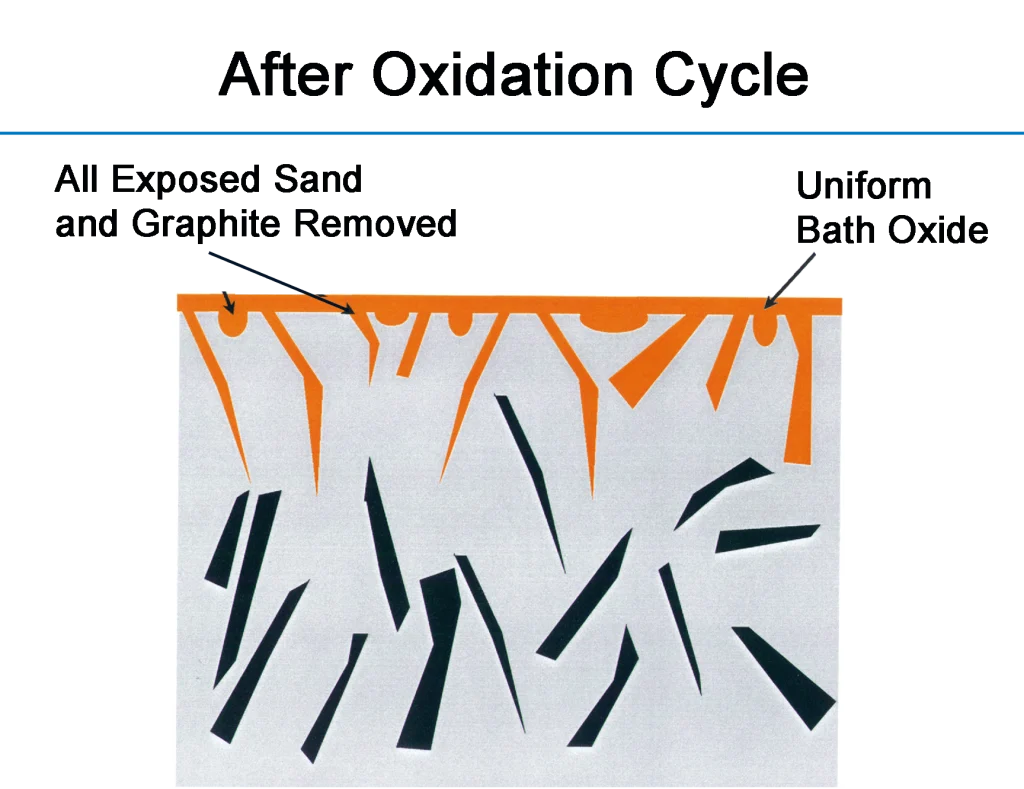
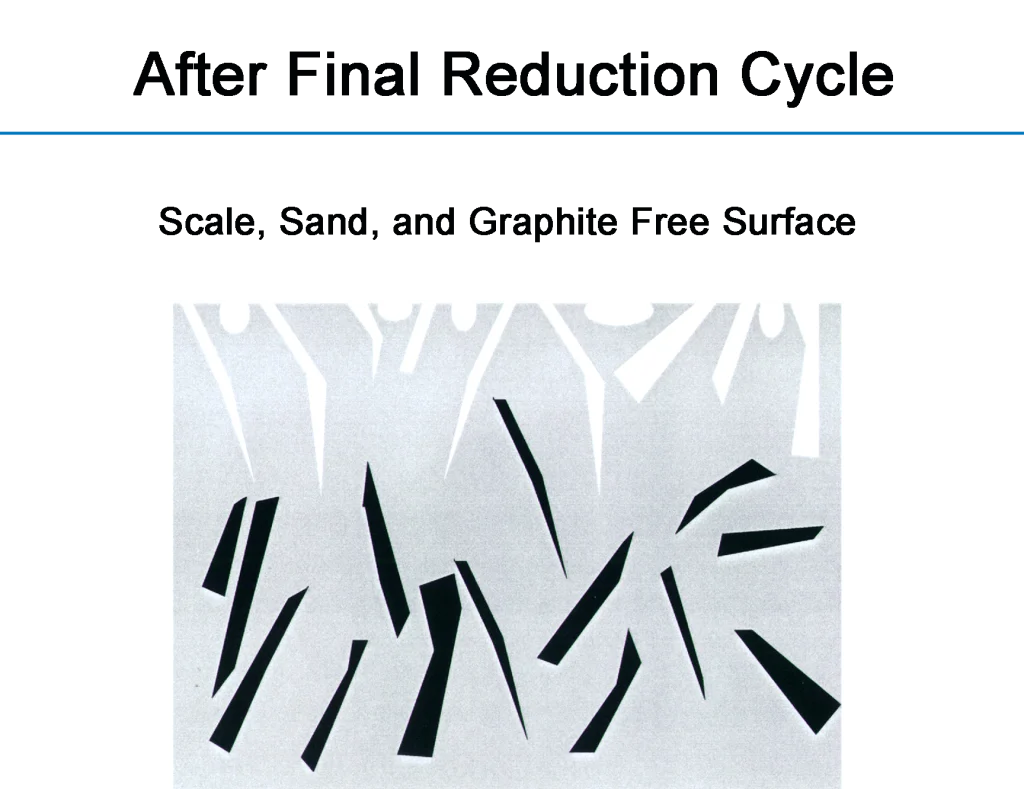
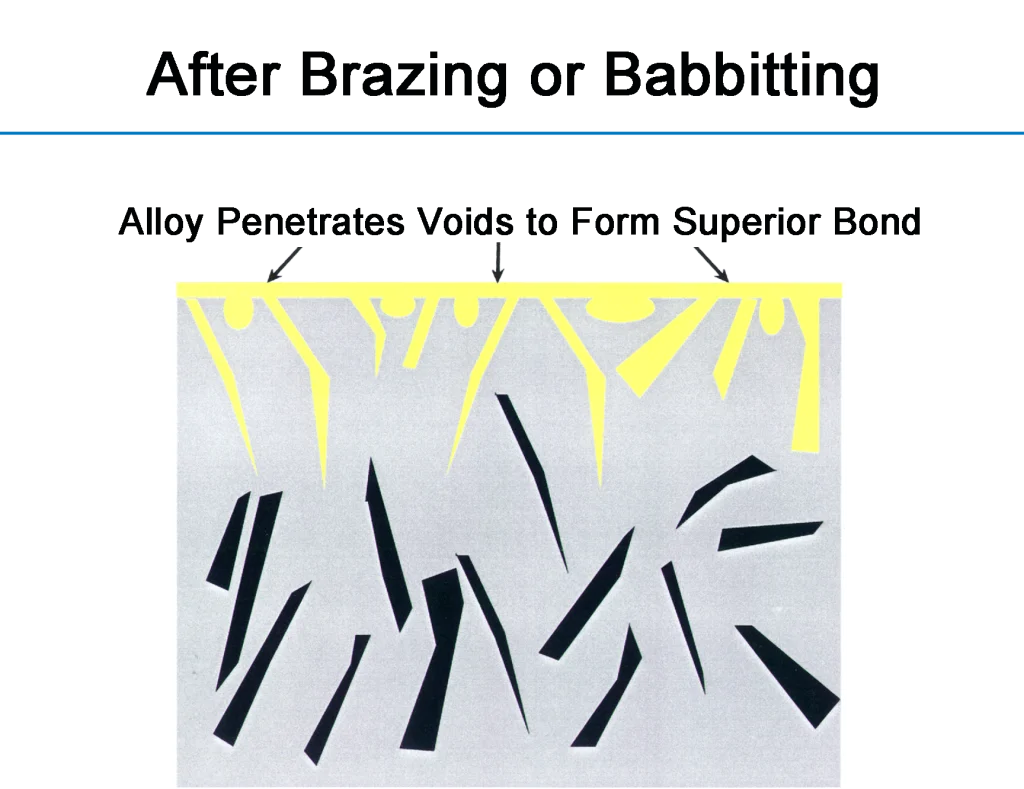
If you are brazing or babbitting iron sand castings, Kastech Electrolytic can greatly improve bond strength and joint integrity. The bath electrochemically oxidizes exposed surface graphite to produce carbon dioxide. At the same time, any casting oxides are gently converted to a uniform ferric oxide.
Once the graphite has been removed, the polarity of the charge is reversed. This reduces the ferric oxide and leaves an oxide-free surface. Any exposed sand is removed simultaneously during both oxidation and reduction cycles.
If you will braze or babbitt to a machined iron surface, we recommend machining before the Kastech Electrolytic process. Machining after salt bath cleaning re-exposes fresh graphite and cancels the bonding benefit.
We also remove sand and graphite from cast iron castings with the Kastech Electrolytic process at our Detroit plant. See Commercial Processing.

Have parts like these? Tell us the alloy, the coating or residue and your volume, and we will recommend a salt, a system or processing at our Detroit plant.